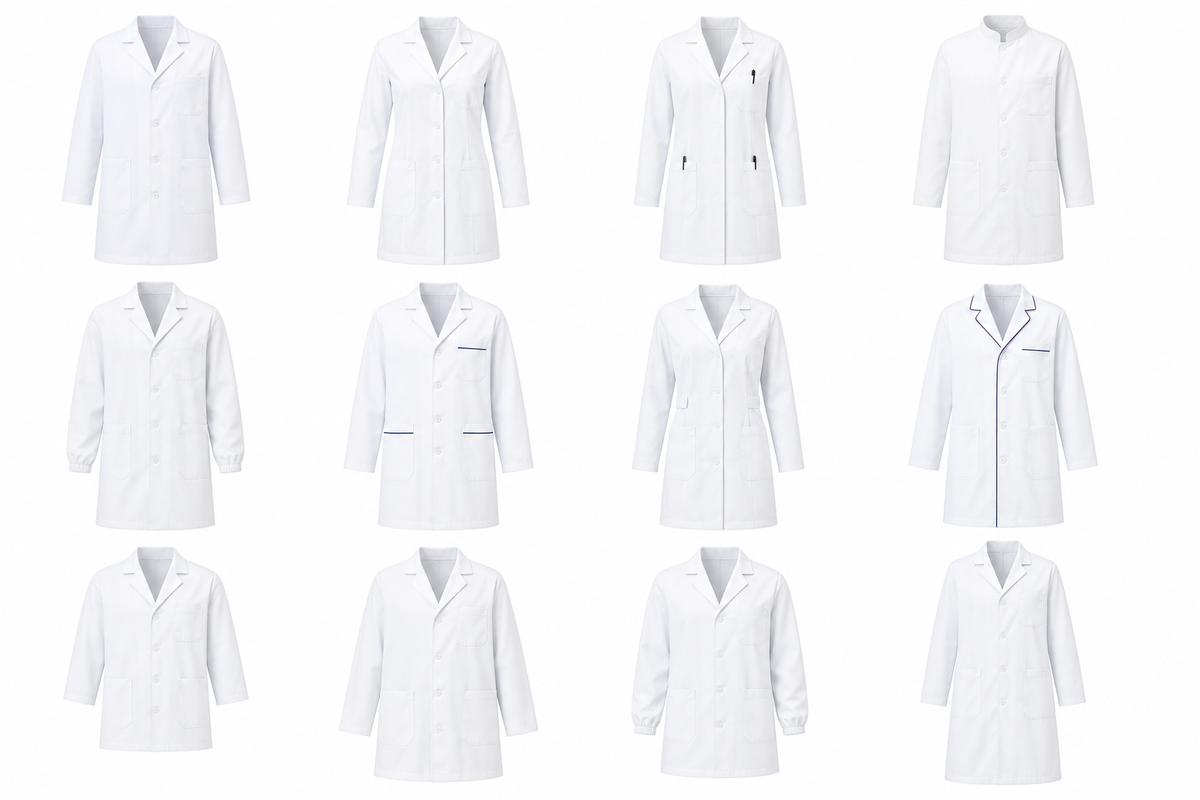
Lab Coat Sourcing & Manufacturing Solutions from China
Your Lab Coat Sourcing Partner
Lab coats represent a critical category in the medical, pharmaceutical, research, and industrial sectors. They serve as essential personal protective equipment, providing barrier protection against chemical splashes, biological contaminants, and particulate matter while maintaining a professional appearance. Manufacturing lab coats demands specific expertise in technical fabrics, seam construction for durability, and quality control that verifies fluid resistance and material integrity.
Our company connects international healthcare brands, hospital procurement departments, pharmaceutical companies, research institutions, and uniform distributors with qualified production facilities across China. We function as a complete sourcing partner, managing every stage from initial design consultation through fabric procurement, sample development, bulk manufacturing, quality verification, and international shipping coordination.
With extensive experience in medical and protective apparel production, we understand what distinguishes this category from standard garment manufacturing. Our network includes factories with specialised equipment for seam sealing, ultrasonic welding, and quality control systems that verify barrier performance and material safety.
Why China Dominates Lab Coat Manufacturing
China continues to dominate the global lab coat supply chain, supported by tightly integrated industrial clusters where raw materials, textile processing, garment assembly, and logistics converge seamlessly . The country's success stems from advanced textile infrastructure, skilled labour, and vertically integrated production ecosystems that enable tight control over quality and cost.
Key Manufacturing Regions for Lab Coats
Hubei Province, particularly Xiantao City, serves as the epicentre of China's non-woven and protective clothing industry. Known as the "Non-Woven Capital of China," Xiantao hosts hundreds of specialised manufacturers benefiting from concentrated expertise in medical textiles and rapid prototyping capabilities . Factories here often operate under strict regulatory standards, making them ideal partners for medical-grade lab coats requiring barrier protection. Suppliers such as Hubei Haixin Protective Products Group Co., Ltd. exemplify the region's strengths, offering ISO-certified production lines and fast response times that support urgent global orders .
Guangdong Province provides superior export infrastructure through major ports such as Guangzhou and Shenzhen. These regions are home to experienced exporters with established freight partnerships, ensuring faster shipping timelines and smoother customs clearance. Guangzhou Care Uniform Co., Ltd., located in the Pearl River Delta, combines strong distribution networks with high-volume output, catering efficiently to international markets .
Jiangsu and Zhejiang Provinces are known for technical textiles and R&D-driven manufacturing. These coastal provinces specialise in functional fabrics with antimicrobial, fluid-resistant, or static-dissipative properties—perfect for medical-grade or cleanroom applications . Factories here offer vertically integrated supply chains, enabling faster turnaround and tighter quality control.
Emerging manufacturing centres in Anhui and Henan provinces offer cost-effective alternatives with lower labour rates and government incentives, translating into lower unit prices without sacrificing essential certifications .
Key Manufacturing Regions for Lab Coats
Hubei Province (Xiantao City): The heart of China's non-woven and protective clothing industry, hosting facilities that often exceed 100,000 m² and serve major international distributors .
Guangdong Province: Coastal powerhouse offering mature supply chains, fast shipping via sea and air, and strong expertise in export logistics—ideal for time-sensitive orders .
Jiangsu & Zhejiang Provinces: Known for technical textiles and antimicrobial/fluid-resistant fabrics, perfect for medical-grade applications .
Manufacturing Services for Lab Coats
We offer three primary manufacturing service models, each designed to accommodate different brand requirements and business stages.
OEM Manufacturing for Lab Coats
Brands with established design specifications benefit from our OEM production service. We manufacture lab coats according to your detailed technical packages, including specific fabric types, size grading, construction methods, and finishing specifications. This service suits companies that have developed their own patterns and simply need reliable manufacturing execution at scale.
ODM Development and Design Support
For brands developing new lab coat collections, our ODM service provides comprehensive development support. We offer an extensive library of existing styles that can be customised with your brand identity. Key design considerations include fabric type, closure options (snap fasteners, concealed zippers, or buttons), pocket configurations, and cuff styles.
Customisation options include:
-
Private label branding on woven labels, printed tags, and care labels
-
Custom embroidery for hospital department identification
-
Personalised hang tags and packaging solutions
-
Fabric selection from a comprehensive range of medical-grade materials
-
Custom size grading for different markets
Private Label Lab Coat Production
Healthcare brands, uniform distributors, and entrepreneurs building medical apparel lines can launch complete collections through our private label manufacturing service. We manage the entire development process from fabric selection and style recommendations through production, quality control, and shipping. This turnkey approach significantly reduces time-to-market and eliminates the technical expertise typically required for production.
Lab Coat Fabric and Material Options
Lab coat performance depends fundamentally on fabric selection. Our manufacturing partners offer access to a comprehensive range of materials suitable for different applications, from standard clinical use to demanding cleanroom environments.
Fabric Categories for Lab Coats
Polyester-Cotton Blends (65/35) represent the industry standard for reusable lab coats, offering the ideal balance of durability, comfort, and easy-care properties . This fabric retains whiteness after 50+ washes using chlorine-based detergents and maintains structural integrity through repeated industrial laundering .
Polypropylene Non-Woven Fabric is the primary material for disposable lab coats, providing cost-effective barrier protection for single-use applications . Available in weights from 45-70 GSM, these fabrics offer varying levels of fluid resistance.
100% Polyester with Conductive Fibres meets the requirements of cleanroom and electrostatic-sensitive environments. Products like those conforming to EN 1149-3 standards provide essential static control and are often autoclavable up to 121°C .
Antimicrobial-Treated Fabrics incorporate silver chloride or other agents to inhibit bacterial growth, increasingly important for infection control in clinical settings .
Fluid-Resistant Fabrics comply with ANSI/AAMI PB70 Levels 1-4 and EN 13795 standards for barrier protection against blood and body fluids.
Trims and Accessories for Lab Coats
-
Snap fasteners and concealed zippers for secure closure
-
Elastic cuffs for a snug fit and contamination prevention
-
Multiple pockets (breast, hip, interior) for practical storage
-
Woven and printed labels with custom branding
Product Range Capabilities
Our manufacturing network produces the complete spectrum of lab coats for medical, pharmaceutical, research, and industrial applications.
-
White Clinical Lab Coats (standard and custom-fit)
-
Medical Doctor Coats and Hospital Uniforms
-
Nurse Uniforms and Clinical Gowns
-
Cleanroom Lab Coats (anti-static, low-lint)
-
Disposable and Single-Use Lab Coats
-
Antimicrobial and Fluid-Resistant Coats
-
Chemical-Resistant Lab Coats
-
Sterile Lab Coats for Aseptic Environments
-
Custom Embroidery and Department Identification Lab Coats
-
Unisex and Gender-Specific Lab Coats
-
Plus Size Lab Coats
-
Children's Lab Coats (educational/science settings)
Production Specifications and Supply Chain Parameters
Quality Assurance for Lab Coats
Lab coats must meet stringent standards for quality, safety, and performance. Our quality assurance system addresses these requirements through comprehensive inspection protocols.
Pre-Production Verification
Before bulk manufacturing commences, we verify that all materials meet specified quality standards. This includes testing fabric composition, colourfastness, seam strength (minimum 20N force resistance), fluid resistance, and antimicrobial effectiveness . For medical-grade products, we confirm compliance with relevant certifications including ISO 13485, EN 13795, and ANSI/AAMI PB70. We confirm that sizing specifications match approved samples and that all construction details are clearly understood by the production team.
In-Line Production Monitoring
During cutting, sewing, and finishing stages, our inspection team conducts systematic checks to verify construction quality. For lab coats, this includes confirming that seams are reinforced at stress points, that snap fasteners and zippers are securely attached, that pocket placement and stitching meet design specifications, and that size grading remains consistent across production runs.
Final Finished Product Inspection
Completed lab coats undergo comprehensive inspection covering:
-
Fabric quality and consistent colour matching
-
Seam construction and reinforcement (minimum 20N force resistance)
-
Fastener security and functionality
-
Pocket construction and placement
-
Interior finish quality and label application accuracy
-
Fit accuracy against size specifications
-
Overall appearance and presentation quality
-
Packaging completeness and labelling accuracy
Pre-Shipment Verification
Before container loading, we conduct final random sample inspection to confirm the entire production batch meets quality standards. Third-party inspection services from accredited agencies such as SGS, Intertek, or TÜV can be arranged for clients requiring independent verification .
Certifications and Compliance Standards
Our manufacturing network includes factories holding relevant international certifications that demonstrate commitment to quality, safety, and social responsibility .
-
ISO 9001: Quality management systems for consistent production processes
-
ISO 13485: Medical device quality management (essential for sterile or clinical environments)
-
EN 13795 / AAMI PB70: Barrier protection standards for fluid resistance
-
OEKO-TEX® Standard 100: Ensures textiles are free from harmful substances
-
ASTM F1670/F1671: Blood and viral penetration testing for fluid resistance
-
REACH Compliance: Chemical safety standards for the EU market
-
BSCI / SMETA Audits: Demonstrate adherence to ethical labour practices
These credentials provide assurance that production processes meet international expectations for quality, safety, and environmental sustainability.
Packaging and Retail Presentation
Lab coat packaging can be tailored to your retail and shipping requirements.
Basic Packaging
-
Custom poly bag with your branding
-
Barcode label and care instructions
-
Size and style labels
Retail-Ready Packaging
-
Branded poly bags with custom printing
-
Hang tags, swing tags, and branding cards
-
Custom printed boxes for premium presentation
-
Eco-friendly packaging options
-
Retail-ready folding techniques
Bulk Shipping Packaging
-
Export cartons with reinforced construction (typically 7-layer corrugated)
-
Palletised packing for container loading
-
Moisture barrier protection for sea freight
-
Clear carton marking with style and size information
All packaging materials can be custom-branded with your logo, colour scheme, and label requirements.
Shipping and Logistics Overview
Lab coat collections often require precise timing for hospital contracts, university orders, or seasonal uniform changes. Our logistics team provides comprehensive shipping solutions tailored to your timeline and budget.
Shipping Timeframes
-
Sea Freight to North America: 12-18 days port-to-port
-
Sea Freight to Europe: 14-20 days
-
Sea Freight to Australia and Asia: 8-14 days
-
Air Freight to Worldwide Destinations: 3-7 days
-
Express Courier Services: 3-5 days door-to-door
Total Lead Time Calculation
Recommended planning allowance from order confirmation to warehouse delivery is approximately 65-85 days when using sea freight. This includes 5-10 days for sample development, 25-40 days for bulk production, and 12-18 days for ocean transport plus customs clearance procedures . Advance planning of at least three months ensures reliable delivery and provides contingency time for unexpected delays.
Proximity to major ports like Shanghai, Shenzhen, and Guangzhou enables faster shipping timelines. Many established suppliers maintain on-time delivery rates exceeding 97% .
Frequently Asked Questions About Lab Coat Sourcing
What MOQ do you require for custom lab coats?
Our standard MOQ is 100 pieces per style per colour. Selected stock items may be available with MOQ as low as 2 pieces for sample validation and test orders . For fully custom OEM/ODM production, MOQ typically starts from 100 pieces.
What fabric options are available for lab coats?
Available materials include polyester-cotton (65/35) blends for reusable coats, polypropylene for disposable options, polyester with conductive fibres for cleanroom environments, and antimicrobial-treated or fluid-resistant fabrics for clinical applications .
What safety certifications do your factories hold?
Our manufacturing partners hold ISO 9001, ISO 13485, OEKO-TEX Standard 100, EN 13795, and BSCI certifications, ensuring compliance with international quality and safety standards .
How long does sample development take?
Sample development typically requires 5-10 working days, depending on design complexity and fabric availability .
What is the typical production timeline?
Bulk production generally takes 25-40 working days from sample approval. Total lead time including shipping ranges from 65-85 days for sea freight .
Do you offer sustainable fabric options?
Yes. We offer eco-friendly options including recyclable materials and OEKO-TEX certified fabrics upon request.
Can you assist with shipping and documentation?
Yes. We arrange international transportation, prepare complete export documentation, and provide customs clearance support when required.
Do you offer third-party inspection services?
Yes. We can arrange third-party inspections from accredited agencies such as SGS, Intertek, or TÜV for clients requiring independent verification .
Getting Started with Your Lab Coat Project
Whether you are sourcing for a hospital network, pharmaceutical company, research institution, or uniform distributor, our team can help you navigate the Chinese manufacturing landscape effectively.
Contact us today with your lab coat specifications. We will respond with a tailored sourcing proposal covering production options, pricing estimates, timeline recommendations, and quality assurance protocols for your specific requirements. Our commitment is to provide professional, reliable sourcing support that helps you bring quality lab coat products to market efficiently and competitively. From medical-grade disposable coats to durable reusable clinical uniforms, we simplify the process and deliver consistent results.